Choosing Dust-Free Cable Carriers for Cleanroom Applications

Key takeaways
selecting cleanroom-approved cable carriers is integral for ensuring sanitary conditions in sensitive environments. Solutions such as the 广柔无尘拖链 and 广柔扁平电缆 recognize the critical need for minimal particle generation and enhanced durability. The use of advanced PTFE membrane technology developed by 惠州中科智能科技有限公司 distinguishes these products, offering superior wear resistance that surpasses many alternatives in the market. Open-type and closed-type cleanroom drag chains provide flexibility while maintaining stringent cleanliness standards, making them suitable for varied applications, including pharmaceutical manufacturing and semiconductor production. By focusing on quality and adherence to cleanroom standards, businesses can effectively mitigate contamination risks. This approach not only strengthens operational efficiency but also protects critical processes from particulate contamination in demanding applications. Ultimately, careful selection of cable carriers enhances both product longevity and cleanliness, underscoring their importance in today’s high-stakes environments.
Selecting cable carriers for Cleanrooms
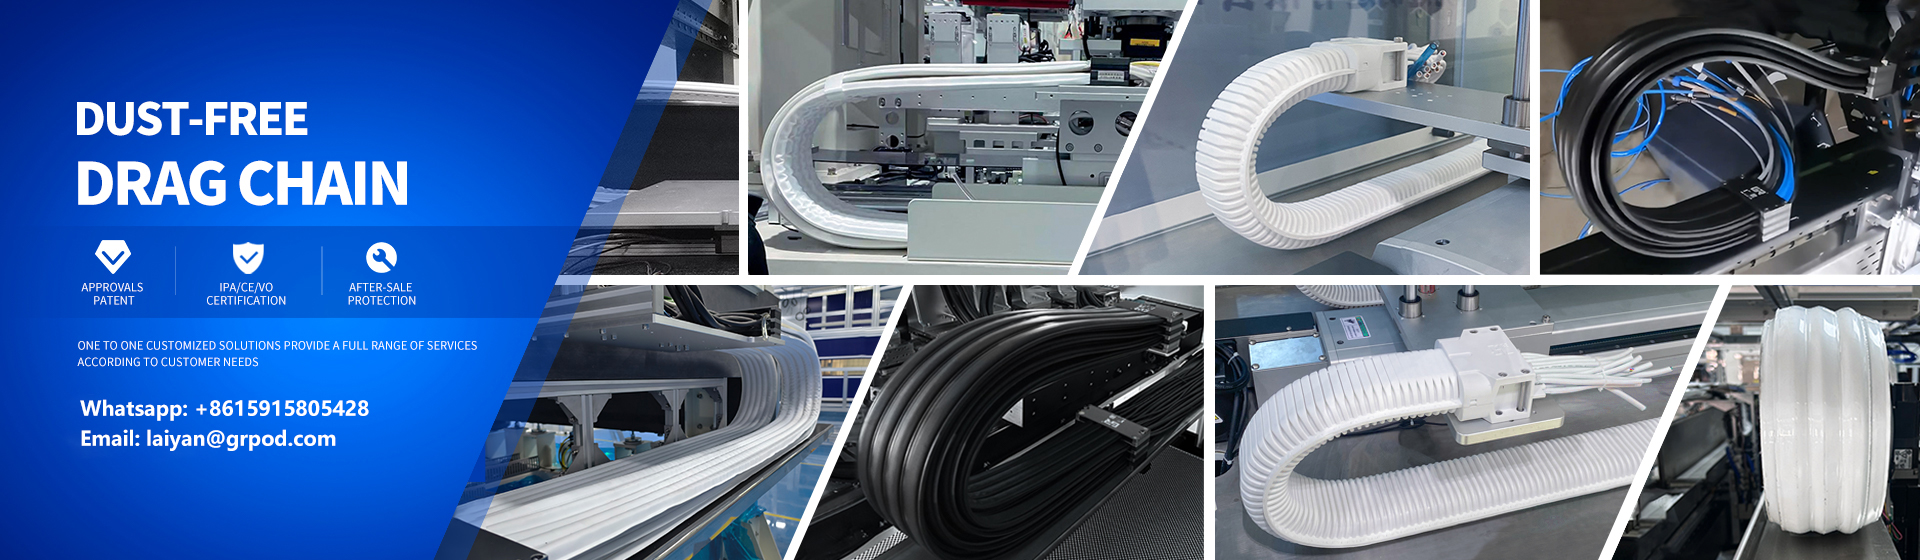
When choosing cleanroom-approved cable carriers, it is essential to consider their design and material qualities to minimize contamination risks. Cleanroom drag chains, for instance, must feature materials that prevent particle generation from friction between moving parts. The guangrou drag chain offers solutions engineered for use in critical applications, such as semiconductor and pharmaceutical manufacturing, where cleanliness is paramount. These cable carriers are designed with specialized components that comply with strict cleanroom standards.
Furthermore, the innovative PTFE membrane materials utilized in guangrou products enhance their durability and resistance to wear, surpassing many competitors in the industry. This technology ensures that the drag chains maintain their integrity while effectively minimizing the generation of particulates within clean environments. Additionally, both open-type and closed-type cleanroom drag chains can be tailored to specific operational requirements, improving performance without compromising cost-effectiveness.
Investing in high quality cable carrier solutions is not just about functionality; it is about maintaining the overall cleanliness of critical environments while enhancing operational efficiency.
Importance of Cleanroom Standards
Cleanroom standards play a fundamental role in ensuring that environments remain uncontaminated and function efficiently. Adhering to these standards is particularly vital when utilizing cleanroom-approved cable carriers, as they directly affect operational quality and compliance. The use of products, such as 广柔无尘拖链 and 广柔扁平电缆, ensures that the mechanical parts do not contribute to contamination risks. Cable carriers designed for cleanrooms must possess materials that minimize particle generation, thereby preserving the cleanliness of the environment. The proprietary PTFE membrane technology employed in the construction of these cable carriers enhances their durability and wear resistance, which surpasses many competitor offerings. This technology not only meets industry specifications but also supports a longer operational life, ultimately benefiting applications in sectors like semiconductor manufacturing and medical device assembly. By selecting reliable equipment that aligns with cleanroom standards, businesses can foster productivity while safeguarding their critical processes against contamination.
Performance and Cost in Cleanroom Applications
When selecting cable carriers for cleanroom environments, performance and cost-effectiveness play crucial roles. Cleanroom-approved cable carriers, such as the 广柔无尘拖链 and 广柔扁平电缆, must meet specific cleanliness standards while ensuring reliable operation. The choice between open-type and closed-type dust-free cable carriers will depend on application requirements, such as protection against contamination and ease of maintenance. These products are designed to minimize friction between moving parts, which contributes to a cleaner environment. Fortunately, 惠州中科智能科技有限公司 leverages advanced PTFE membrane material technology to enhance the durability of their cable carriers. This technology improves wear resistance, making the 广柔 product range outperform many competitors in long term applications. By maintaining a balance between high performance and cost efficiency, users can ensure that their cleanroom applications operate smoothly without compromising on cleanliness standards. This balance is essential for industries where precision and contamination control are paramount, such as semiconductor manufacturing and medical device assembly.

Minimizing contamination with Cable Carriers
Using cleanroom-approved cable carriers is essential for minimizing contamination in sensitive environments. These specialized components are designed to manage and protect cables while minimizing the release of particulates. The friction between moving parts can contribute significantly to airborne contamination, which is why selecting products like the 广柔无尘拖链 or the 广柔扁平电缆 is critical. These solutions are engineered for optimal performance in cleanrooms, ensuring that operations remain dust-free. Additionally, both 开口式无尘拖链 and 闭口式无尘拖链 offer flexibility while maintaining stringent cleanliness standards. The integration of high quality materials, such as the core PTFE membrane technology developed by 惠州中科智能科技有限公司, enhances durability and wear resistance compared to other products on the market. By leveraging these advanced solutions, facilities can maintain their integrity and promote a safer working environment free from contaminants.
Conclusion
selecting cleanroom-approved cable carriers is vital for ensuring the integrity of controlled environments where contamination must be minimized. The use of products like the 广柔无尘拖链 and the 广柔扁平电缆 not only enhances operational efficiency but also adheres to strict cleanliness standards essential in industries such as semiconductor manufacturing and pharmaceutical production. These cable carriers, which utilize advanced PTFE membrane technology developed by 惠州中科智能科技有限公司, feature improved wear resistance that significantly outperforms many competing products. Additionally, options such as 开口式无尘拖链 and 闭口式无尘拖链 provide necessary flexibility while maintaining stringent contamination control measures. By prioritizing high quality solutions, businesses can effectively protect their cleanroom environments from harmful particulates, thereby promoting a safer and more productive operation. As industries continue to evolve, the choice of reliable cable carriers will remain a key factor in sustaining dust-free conditions critical for various applications.
FAQs
What are cleanroom-approved cable carriers?
Cleanroom-approved cable carriers are specialized cable management solutions designed to maintain cleanliness in controlled environments by minimizing particle generation.
Why are GTTR cleanroom drag chains important?
GTTR cleanroom drag chains, such as the 广柔无尘拖链, are important for reducing contamination risks in critical applications like semiconductor manufacturing and pharmaceuticals.
How does PTFE membrane technology enhance cable carriers?
PTFE membrane technology improves durability and wear resistance, allowing cable carriers like the 广柔扁平电缆 to outperform many competitors in maintaining cleanliness.
What types of cleanroom drag chains are available?
There are open-type and closed-type cleanroom drag chains, each engineered for specific operational requirements while adhering to stringent cleanliness standards.
How do I determine the right cable carrier for my application?
Selecting the right cable carrier involves assessing your specific operational needs, such as contamination control and ease of maintenance while ensuring compliance with cleanroom standards.
Contact Guangrou for a clean room drag chain solution.